Statistical process control is a quality method that uses control charts and basic statistics to monitor a process while it runs, separating the normal variation every process shows from genuine problems that need action, so teams can catch defects at the source instead of sorting them out after the parts are already made.
In the systems we build for aerospace and manufacturing clients, SPC is rarely the hard part. The hard part is choosing the right characteristic to chart, reacting to the correct signals, and connecting the chart back to the control plan so an operator knows exactly what to do when a point falls out of limits. Get those three things right and the math takes care of itself.
Key takeaways
- SPC watches a live process with control charts, not finished parts with an inspection gate.
- Control limits describe what the process actually does; specification limits describe what the customer wants. They are not the same thing.
- Common cause variation is the process being itself; special cause variation is a signal that something changed.
- Cp and Cpk turn that stable behavior into a capability number you can put in front of an auditor or a customer.
How statistical process control actually works
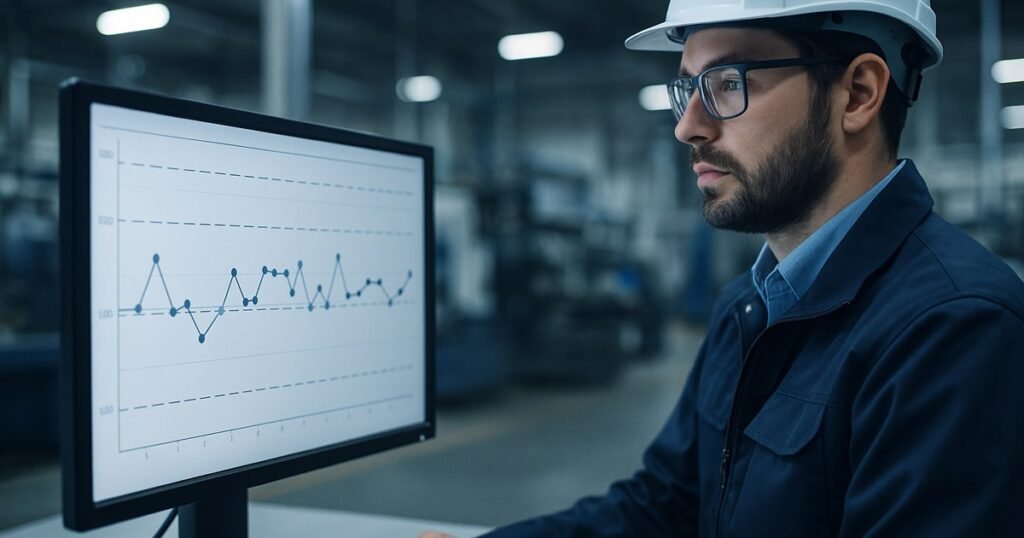
Statistical process control starts with a measurable characteristic that matters, a bore diameter, a torque value, a coating thickness. You sample the process at set intervals, plot each result on a control chart, and compare it against control limits calculated from the process data itself. Those limits usually sit at plus or minus three standard deviations from the process average, which captures about 99.7 percent of normal output.
The point people miss is that control limits are not the same as tolerance. Control limits come from the voice of the process. Specification limits come from the voice of the customer. A process can sit comfortably inside its control limits and still make out-of-spec parts, which is exactly why capability analysis exists as a separate step.
Common cause vs special cause variation
Every process varies. The whole job of SPC is telling the two kinds of variation apart, because they call for completely different responses.
| Type | What it is | What to do |
|---|---|---|
| Common cause | The natural, always-present variation built into the process: minor material differences, small machine play, ambient conditions. | Leave it alone. Chasing individual points makes it worse. Improve it by changing the process itself. |
| Special cause | Variation from a specific, assignable event: a new material lot, a worn tool, a setup error, an operator change. | Investigate now, find the root cause, and correct it before it produces scrap. |
Reacting to common cause as if it were a signal is called tampering, and it reliably increases variation. That single distinction is the reason SPC saves money instead of just generating paperwork.
Control charts and the 7 rules of SPC
A control chart is a run chart with a center line and control limits added. To read one consistently, most teams use a set of pattern rules, often called the seven rules or the Western Electric and Nelson rules. Common signals include:
- A single point outside the upper or lower control limit.
- Nine points in a row on the same side of the center line.
- Six points in a row steadily increasing or decreasing.
- Fourteen points alternating up and down.
- Two of three points near the same three-sigma edge.
- Four of five points beyond one sigma on one side.
- Fifteen points in a row hugging the center line, which often means the limits are wrong or the data is being filtered.
You do not need all seven on day one. Start with the first three, train operators to trust them, and add the rest once the shop floor is comfortable acting on a signal without second-guessing it.
Cp and Cpk: measuring process capability
Once a process is stable and in control, capability indices tell you whether it can actually hold tolerance. Cp compares the spread of the process to the width of the specification, assuming the process is centered. Cpk does the same but accounts for how far off-center the process runs, so it is the more honest number. A Cpk of 1.33 is a common minimum for aerospace and automotive characteristics, and many customers ask for 1.67 on critical features. A high Cp with a low Cpk is the classic sign of a capable process that simply needs re-centering.
Is SPC part of Six Sigma?
Yes. SPC predates Six Sigma by decades, but it lives inside the Control phase of the DMAIC framework, where control charts hold onto the gains a project delivers. SPC is also one of the seven basic quality tools, alongside the Pareto chart, fishbone diagram, histogram, check sheet, scatter diagram, and flowchart. You can run SPC without ever launching a Six Sigma project, and most manufacturers do.
How SPC connects to the control plan and PFMEA
This is where statistical process control stops being a standalone chart and becomes part of a real quality system. Your PFMEA identifies the process steps most likely to fail and how badly it hurts if they do. Those high-risk characteristics flow directly into the control plan, which names the control method for each one, and for the critical few that method is SPC. The control chart then feeds evidence back: if a special cause keeps appearing, that is a signal to revisit the PFMEA risk ranking. When SPC, the control plan, and the APQP planning documents point at the same characteristics, an audit becomes a straightforward conversation instead of a scramble.
The OQS SPC rollout checklist
Across the programs we set up, these five steps separate SPC that works from SPC that gathers dust:
- Chart the vital few, not everything. Pull characteristics straight from the PFMEA and control plan. Ten meaningful charts beat a hundred nobody reads.
- Prove the measurement first. Run a gauge R and R before you trust a chart. If the measurement system is noisy, the chart is fiction.
- Write the reaction on the chart. Every chart needs a documented reaction plan so the operator knows who to call and what to quarantine when a point goes out.
- Recalculate limits after real change. New tooling, new material, or a validated improvement means new control limits, not the old ones carried forward out of habit.
- Review capability on a cadence. Track Cpk over time, not once at part approval, so drift shows up before the customer finds it.
Statistical process control FAQ
What are the 7 tools of SPC? The seven basic quality tools are the control chart, Pareto chart, cause-and-effect (fishbone) diagram, histogram, check sheet, scatter diagram, and flowchart. The control chart is the tool most people mean when they say SPC.
What are the 5 steps of the statistical process? Identify the characteristic to monitor, verify the measurement system, collect data and calculate control limits, plot and interpret the chart against the rules, and act on special causes while working to reduce common cause variation.
Is SPC a Six Sigma tool? It is one of the seven basic quality tools and the backbone of the Control phase in DMAIC, so it is used heavily in Six Sigma without belonging exclusively to it.
Where can I find the standard reference? The AIAG SPC reference manual is the accepted industry guide for automotive and aerospace supply chains. If you want help turning it into charts your operators will actually use, talk to our team.
Ready to build an audit-ready SPC and quality system?
Optimal Quality Solutions helps aerospace, defense and manufacturing teams build audit-ready quality systems, with a 98% first-time certification success rate and 15+ years of hands-on experience.